Email: info@mggpacking.com | Tel: +86-13510174848 ( Mr. Yao)


How precision engineering and strict quality standards protect your pharmaceutical products every step of the way
When you pick up a bottle of medication from your pharmacy, you probably don't spend much time thinking about the small plastic cap on top. But that tiny component is actually a critical line of defense between your medicine and the outside world. Imagine a scenario where a pill bottle's cap fails to seal properly: moisture creeps in, altering the chemical composition of the tablets inside. Or worse, the contents leak out during transport, rendering the medication useless. For pharmaceutical companies, these aren't just hypothetical risks—they're daily concerns that can compromise patient safety, damage brand reputation, and lead to costly product recalls.
This is where moisture-proof disc caps with anti-leak technology come into play. Designed specifically for the unique demands of the pharmaceutical industry, these caps are engineered to create an airtight, moisture-resistant seal that keeps medications stable from production to patient use. And when they're backed by GMP certification and ISO 9001 standards, you can trust that every cap has been tested, inspected, and manufactured to the highest possible quality benchmarks.
Did you know? Even a 0.1mm gap in a bottle cap can allow enough moisture to enter over time, reducing the shelf life of moisture-sensitive medications by up to 40%. For drugs like antibiotics or vitamins, this isn't just a quality issue—it's a patient safety concern.
At first glance, a disc top cap might seem simple: a plastic lid with a small flip-open nozzle that you press to dispense the product. But under the surface, there's a surprising amount of engineering that goes into making it moisture-proof and leak-resistant. Let's break down the key features that set our caps apart from generic options on the market.
The heart of our moisture-proof design lies in the multi-layer sealing system. Each cap is fitted with an aluminum foil liner that's bonded to a food-grade plastic layer. When the cap is screwed onto the bottle, the liner compresses against the bottle's rim, creating a tight seal that blocks both moisture and oxygen. Unlike single-layer liners, which can degrade over time or crack under pressure, our dual-layer design maintains its integrity even after repeated opening and closing.
We also use a precision-machined threading system (available in sizes like 24/410 and 28/410) that ensures the cap screws on evenly, eliminating gaps that could let moisture seep in. During testing, we subject these caps to extreme conditions—high humidity, temperature fluctuations, and drop tests—to ensure they maintain their seal no matter what the supply chain throws at them.
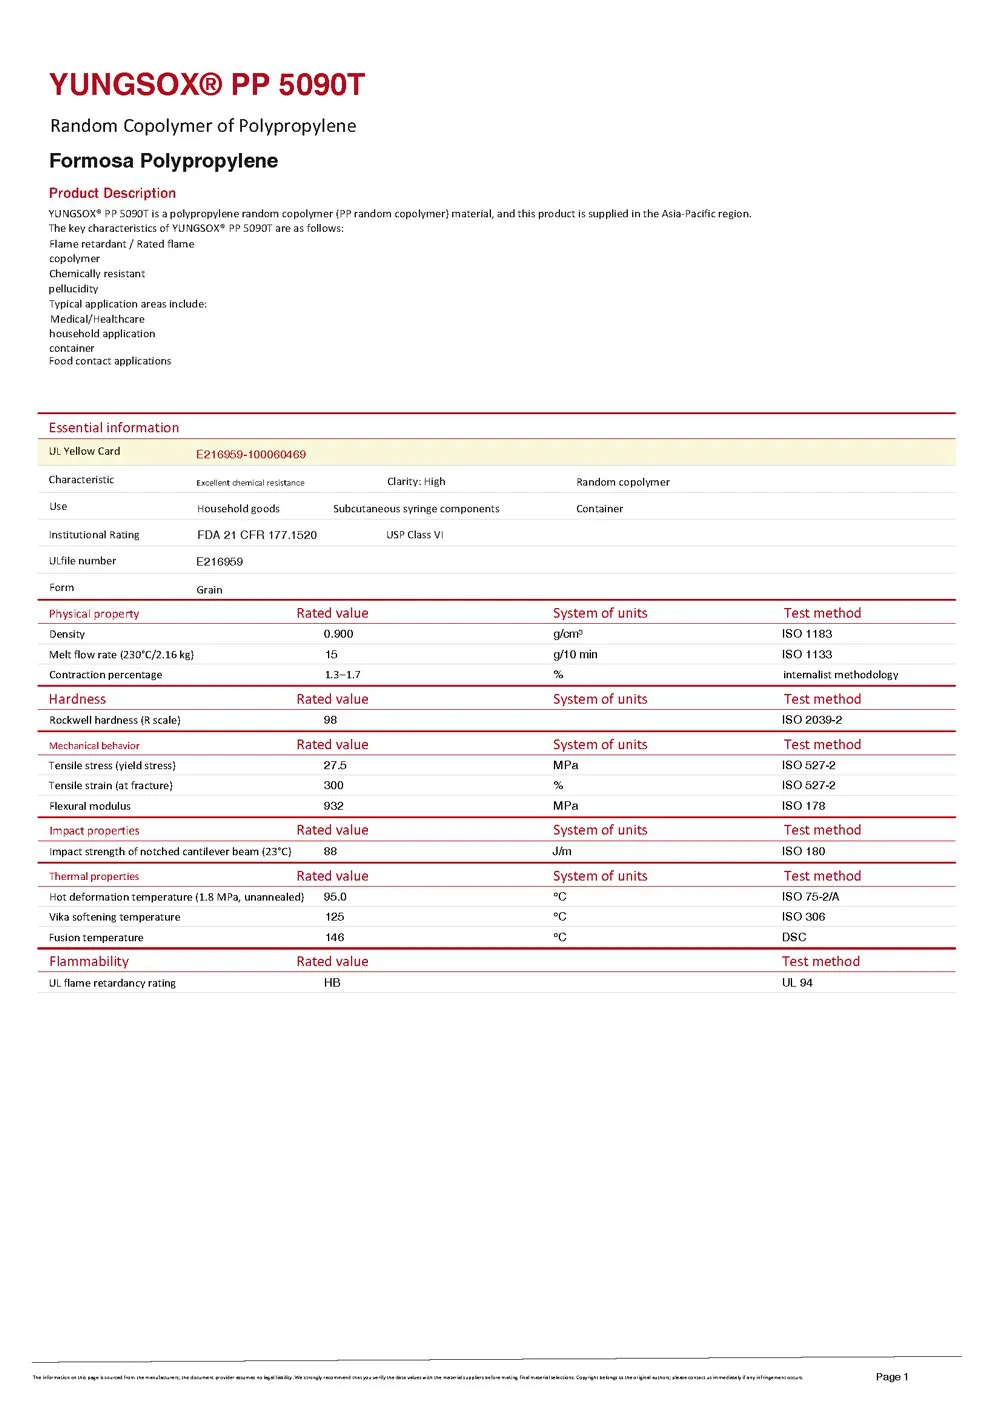
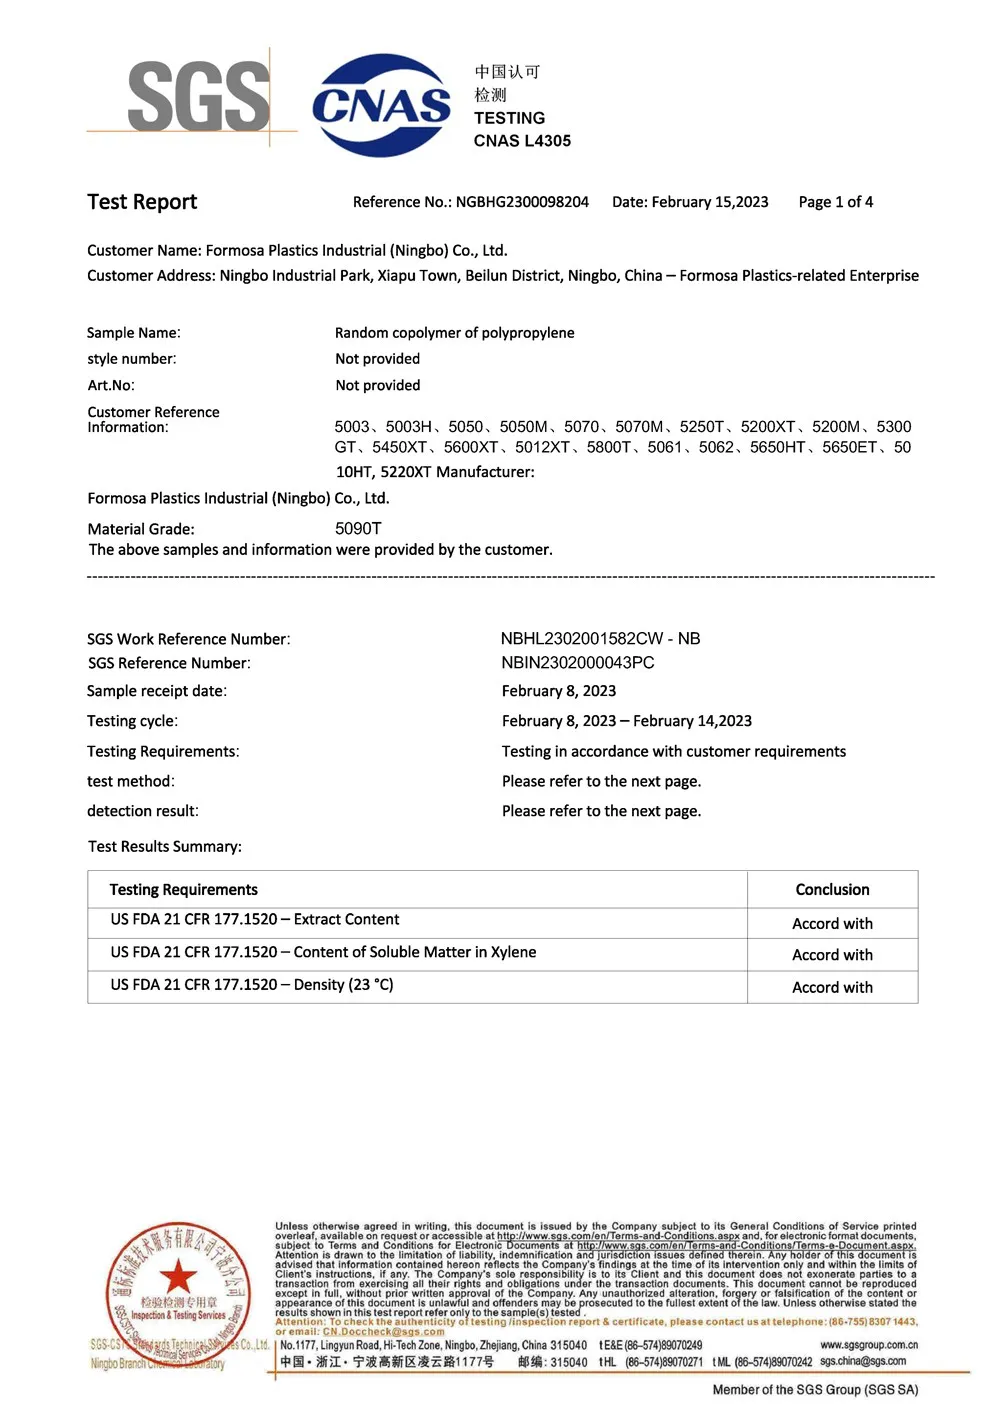
Not all plastics are created equal, especially when it comes to pharmaceutical packaging. That's why we only use medical-grade HDPE (High-Density Polyethylene) and PP (Polypropylene) for our disc caps. These materials are non-toxic, chemical-resistant, and won't leach harmful substances into the medication—critical properties for products that come into direct contact with drugs.
HDPE, in particular, is ideal for pharmaceutical applications because of its low permeability to moisture and gases. It's also lightweight yet durable, making it perfect for both small pill bottles and larger containers. And because we control the entire manufacturing process—from raw material selection to final assembly—we can guarantee that every cap meets the strictest medical-grade standards.
Leakage isn't just a problem during shipping—it can also happen when patients carry medication in their bags or purses. Our disc caps address this with a unique "double-lock" mechanism: the flip-top nozzle snaps shut with an audible click, and a secondary silicone gasket inside the cap adds an extra layer of protection against leaks. Whether the bottle is stored upright, on its side, or even upside down, the contents stay where they belong—inside the bottle.
We recently worked with a client who manufactures liquid cough syrup to test this feature. They subjected our caps to a 24-hour "tumble test," where bottles were rotated and shaken continuously. The result? Zero leakage, even when the bottles were opened and closed multiple times during the test. For pharmaceutical companies, this kind of reliability isn't just a selling point—it's a regulatory requirement.
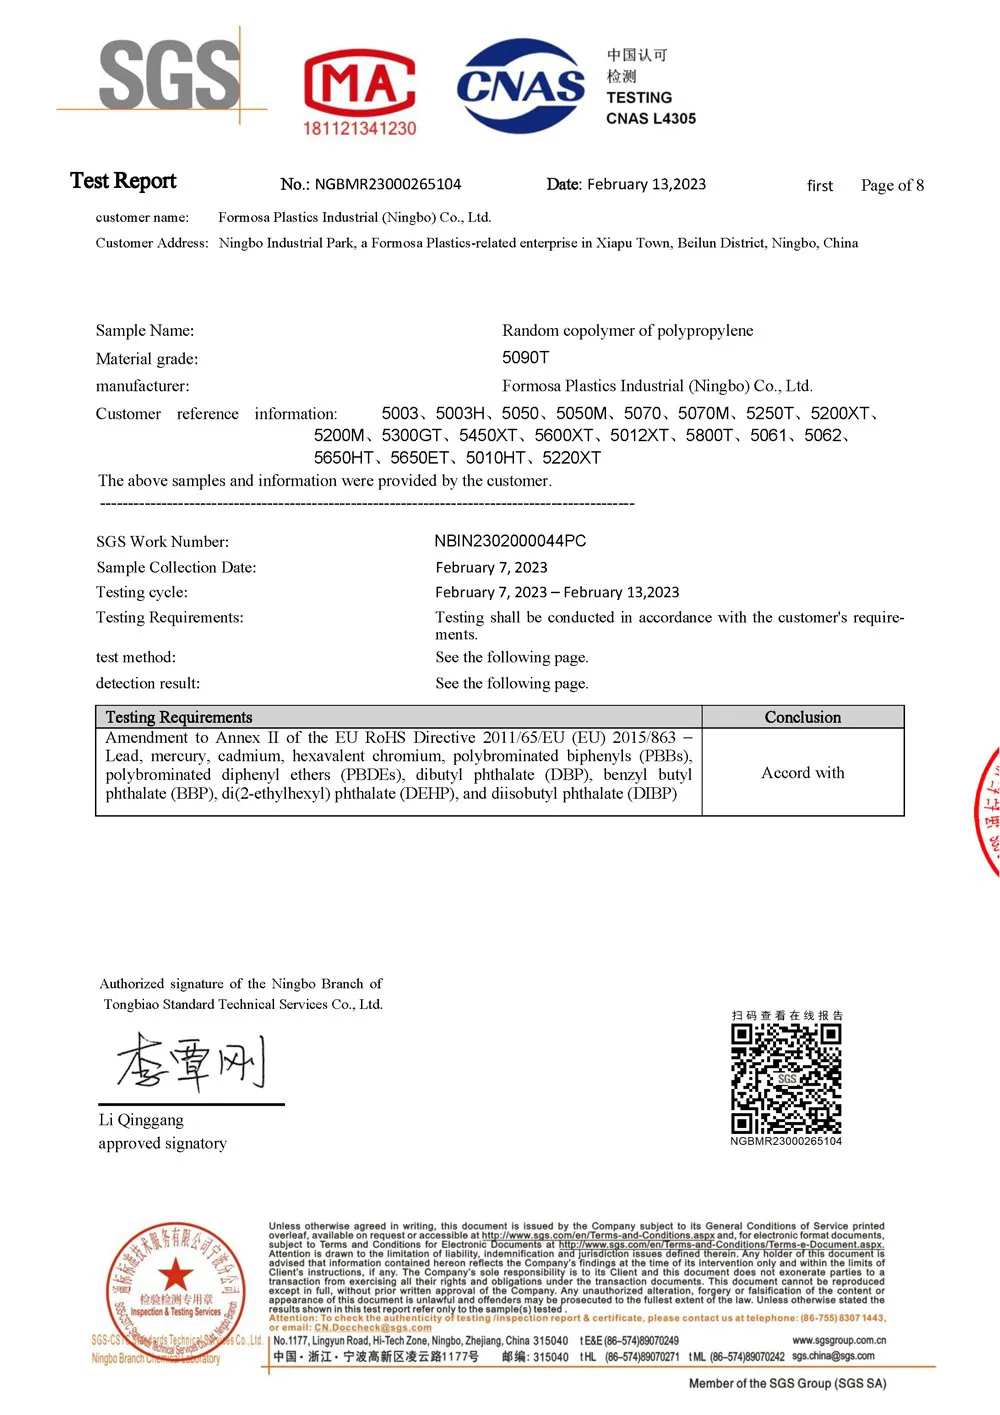
When you see "GMP certified" or "ISO 9001 certified" on a product, what does that really mean? For us, it's not just about hanging a certificate on the wall—it's about embedding quality into every step of the manufacturing process. Let's take a closer look at what these certifications entail and why they matter for pharmaceutical packaging.
GMP, or Good Manufacturing Practices, is a set of guidelines that ensure products are consistently produced and controlled according to quality standards. For pharmaceutical packaging, this means manufacturing in a dust-free, controlled environment where the risk of contamination is minimized. Our workshop is designed with HEPA filtration systems, positive air pressure, and regular cleaning protocols to maintain a Class 8 cleanroom standard—meaning fewer than 100,000 particles (0.5 microns or larger) per cubic foot of air.
What does this look like in practice? Every employee wears head-to-toe protective gear, including hairnets, face masks, and coveralls, to prevent human contamination. Equipment is sanitized daily using FDA-approved disinfectants, and raw materials are stored in sealed containers until they're ready for use. Even the air temperature and humidity are tightly controlled to prevent moisture from affecting the plastic during production.
"We once had a client who visited our workshop and was surprised by how strict our protocols are. They told us, 'We've toured other factories, but none of them paid this much attention to cleanliness.' That's when we knew our commitment to GMP wasn't just meeting standards—it was exceeding them."
ISO 9001 is an international standard that sets out the criteria for a quality management system. For us, this means having documented processes for everything from raw material testing to final inspection, and a system for tracking every batch of caps from production to delivery. If a customer ever has a question about a specific order, we can trace it back to the exact raw materials used, the machine it was produced on, and the operator who inspected it.
One of the key benefits of ISO 9001 is continuous improvement. We regularly review our processes, gather feedback from customers, and conduct internal audits to identify areas where we can do better. For example, after a customer mentioned that some caps were slightly difficult to open, we adjusted the hinge design to make the flip-top easier to use while maintaining the same level of leak resistance. That's the power of a quality management system—it keeps us focused on evolving with our customers' needs.
No two medications are the same, so why should their packaging be? That's why we offer custom mold design services to create disc caps that fit your unique bottle shapes, sizes, and branding needs. Whether you need a cap with a specific color, a custom logo embossed on the top, or a unique threading size to match an existing bottle, our in-house design team can turn your vision into reality.
The process starts with your requirements. Maybe you have a 3D drawing of the bottle you're using, or perhaps you need help designing the cap from scratch. Our team of engineers will work with you to create a digital prototype, which we'll refine until it meets your specifications. Once the design is approved, we'll build a test mold—at no cost to you—to produce a small batch of caps for testing. This allows you to check the fit, seal, and functionality before committing to a full production run.
We recently partnered with a pharmaceutical company that needed a custom cap for their new line of pediatric medications. The bottle was smaller than standard sizes, and they wanted a cap that was easy for parents to open but still child-resistant. Our team designed a 20/410 disc cap with a textured grip and a modified hinge that required a slight squeeze to open—making it simple for adults but difficult for small children. After testing the prototype, they ordered 500,000 caps, and we've been their go-to supplier ever since.
| Customization Option | Benefits | Common Applications |
|---|---|---|
| Color Matching (Pantone Codes) | Aligns with brand identity; makes products instantly recognizable on shelves | Branded over-the-counter medications, vitamin bottles |
| Embossed Logos | Adds a premium, professional look; prevents counterfeiting | Prescription medications, high-end supplements |
| Custom Thread Sizes (e.g., 24/415, 28/415) | Fits unique bottle designs; ensures a secure seal for non-standard shapes | Specialized medical containers, liquid medication bottles |
| Child-Resistant Features | Meets regulatory requirements for hazardous medications | Narcotics, strong painkillers, chemotherapy drugs |
The best part? Our custom mold design service doesn't mean longer lead times. We understand that pharmaceutical companies often work on tight schedules, so we've streamlined our process to deliver test molds in as little as 10 days and full production runs in 3–4 weeks. For urgent orders, we can even expedite the process to meet your deadlines.
While our moisture-proof disc caps are a standout product, we know that pharmaceutical packaging is about more than just caps. That's why we offer a full range of medical-grade plastic bottles and containers to pair with our caps, creating a seamless, end-to-end packaging solution. Whether you need HDPE pill bottles for solid medications, cryogenic tubes for laboratory samples, or custom-shaped containers for liquid drugs, we've got you covered.
Our HDPE pill bottles are designed to work hand-in-hand with our disc caps, creating a complete moisture-resistant package. Made from medical-grade HDPE, these bottles are lightweight, shatterproof, and resistant to chemicals—ideal for storing everything from tablets and capsules to powders and granules. They're also available in a range of sizes, from small 30ml sample bottles to large 500ml containers, and can be customized with features like child-resistant caps, tamper-evident seals, or printed labels.
One of our long-term clients is a vitamin manufacturer who uses our 120ml HDPE bottles with 24/410 disc caps. They love that the combination keeps their vitamins fresh for up to 24 months, even in humid climates. "We used to get complaints about vitamins clumping together," they told us. "Since switching to your bottles and caps, those complaints have dropped to zero."
Sustainability is no longer a trend in packaging—it's a necessity. That's why we're investing in eco-friendly materials and processes to reduce our environmental impact. Our PCR (Post-Consumer Recycled) plastic options allow customers to use bottles and caps made from 30–50% recycled material without compromising on quality or performance. We're also exploring biodegradable plastics for certain applications, though we're careful to ensure these materials still meet medical-grade standards for safety and stability.
For pharmaceutical companies looking to reduce their carbon footprint, we offer lightweighting options—designing bottles and caps with thinner walls that use less plastic while maintaining strength. We recently helped a client reduce their plastic usage by 15% on a 250ml pill bottle, resulting in lower shipping costs and a smaller environmental footprint. It's a win-win: better for the planet, and better for their bottom line.
With so many packaging suppliers on the market, what makes us the right choice for your pharmaceutical needs? It comes down to three things: expertise, reliability, and a commitment to partnership. We've been manufacturing plastic packaging for over 15 years, and in that time, we've learned that pharmaceutical companies need more than just a supplier—they need a partner who understands their unique challenges and can grow with them.
Our team includes engineers with decades of experience in medical packaging, quality control specialists who inspect every batch of caps, and customer service representatives who are available 24/7 to answer questions or address concerns. We don't just sell products—we provide solutions, whether that means helping you navigate regulatory requirements, optimizing your packaging for cost efficiency, or developing a custom design that sets your product apart.
Ready to experience the difference that GMP-certified, moisture-proof disc caps can make for your pharmaceutical products? Contact us today to discuss your needs, request a sample, or start designing your custom mold. With our expertise and commitment to quality, you can trust that your medications will be protected every step of the way.
At the end of the day, pharmaceutical packaging is about more than just holding a product—it's about protecting patients, ensuring efficacy, and building trust. With our moisture-proof disc caps, GMP-compliant manufacturing, and dedication to quality, we're proud to be a partner in that mission.