Email: info@mggpacking.com | Tel: +86-13510174848 ( Mr. Yao)


Crafting Safe, Reliable Packaging for Life-Saving Medications Since 2005
Let's be honest – when you pick up a pill bottle from your local pharmacy, you're not just holding a container. You're holding a promise: that the medication inside stays potent, pure, and protected from the moment it leaves the factory until it reaches your hands. For over 18 years, we've taken that promise seriously. As a leading pharmaceutical packaging manufacturer based in Guangdong, China, we've built our reputation by putting safety, precision, and partnership at the heart of everything we do. Today, our HDPE pill bottles, cryogenic tubes, and custom pharmaceutical containers are trusted by drug companies, supplement brands, and research labs in over 40 countries. This isn't just about making plastic bottles – it's about being a critical link in the healthcare chain.
Here's the thing about pharmaceutical packaging: it's not optional to cut corners. A single flaw in a bottle cap or a tiny crack in the plastic could compromise a medication's efficacy, or worse, put patients at risk. That's why the world's most discerning drug manufacturers don't just "buy" packaging – they partner with suppliers who share their commitment to excellence. Let's break down what makes our HDPE pill bottles stand out.
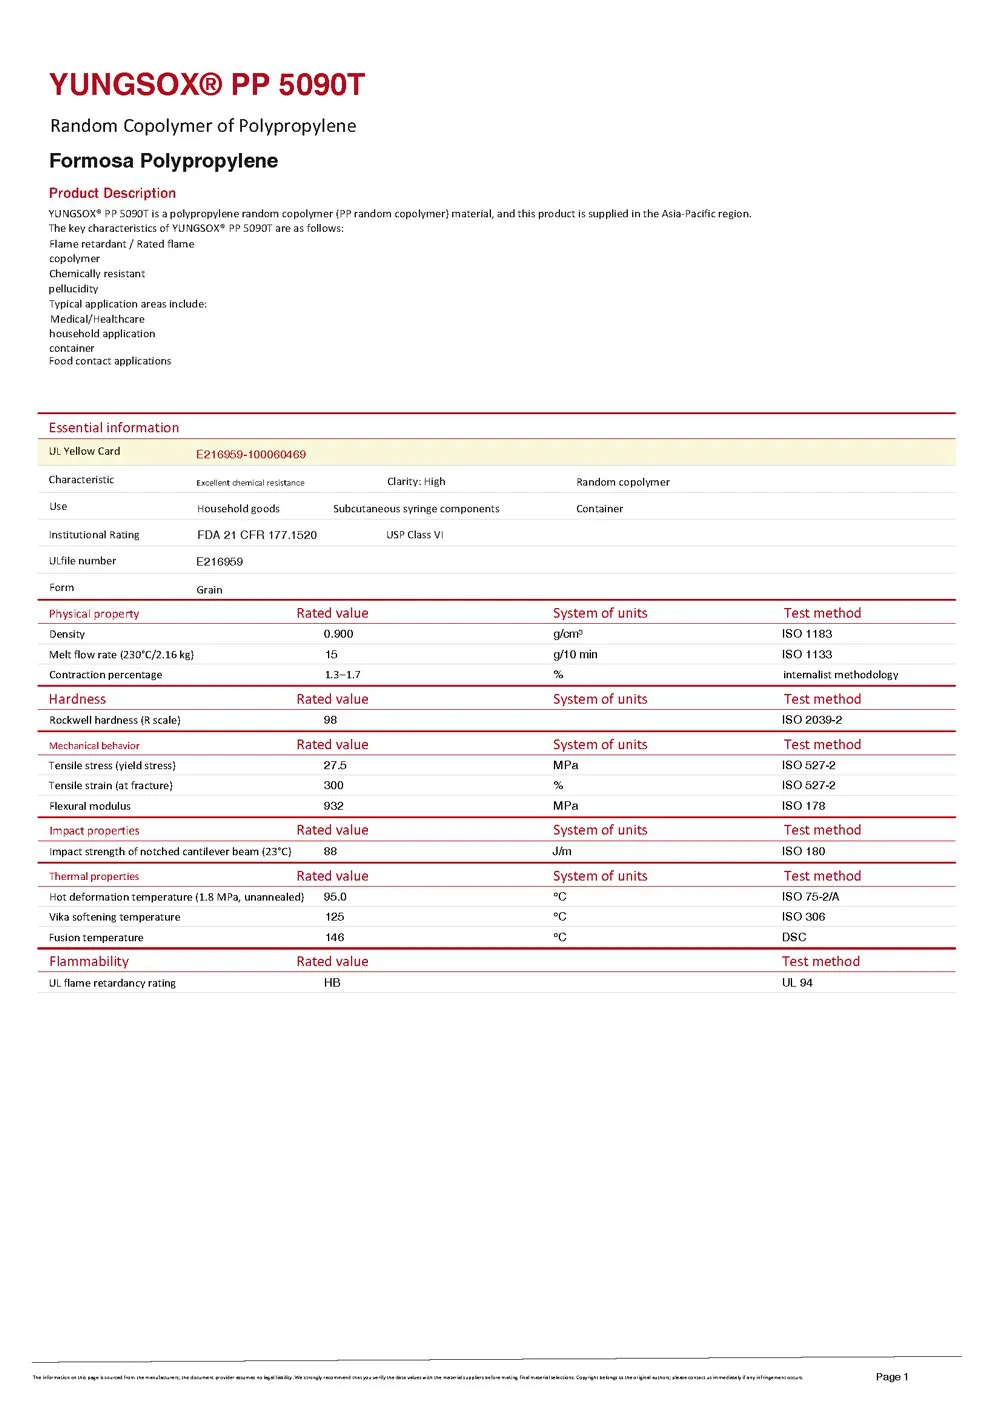
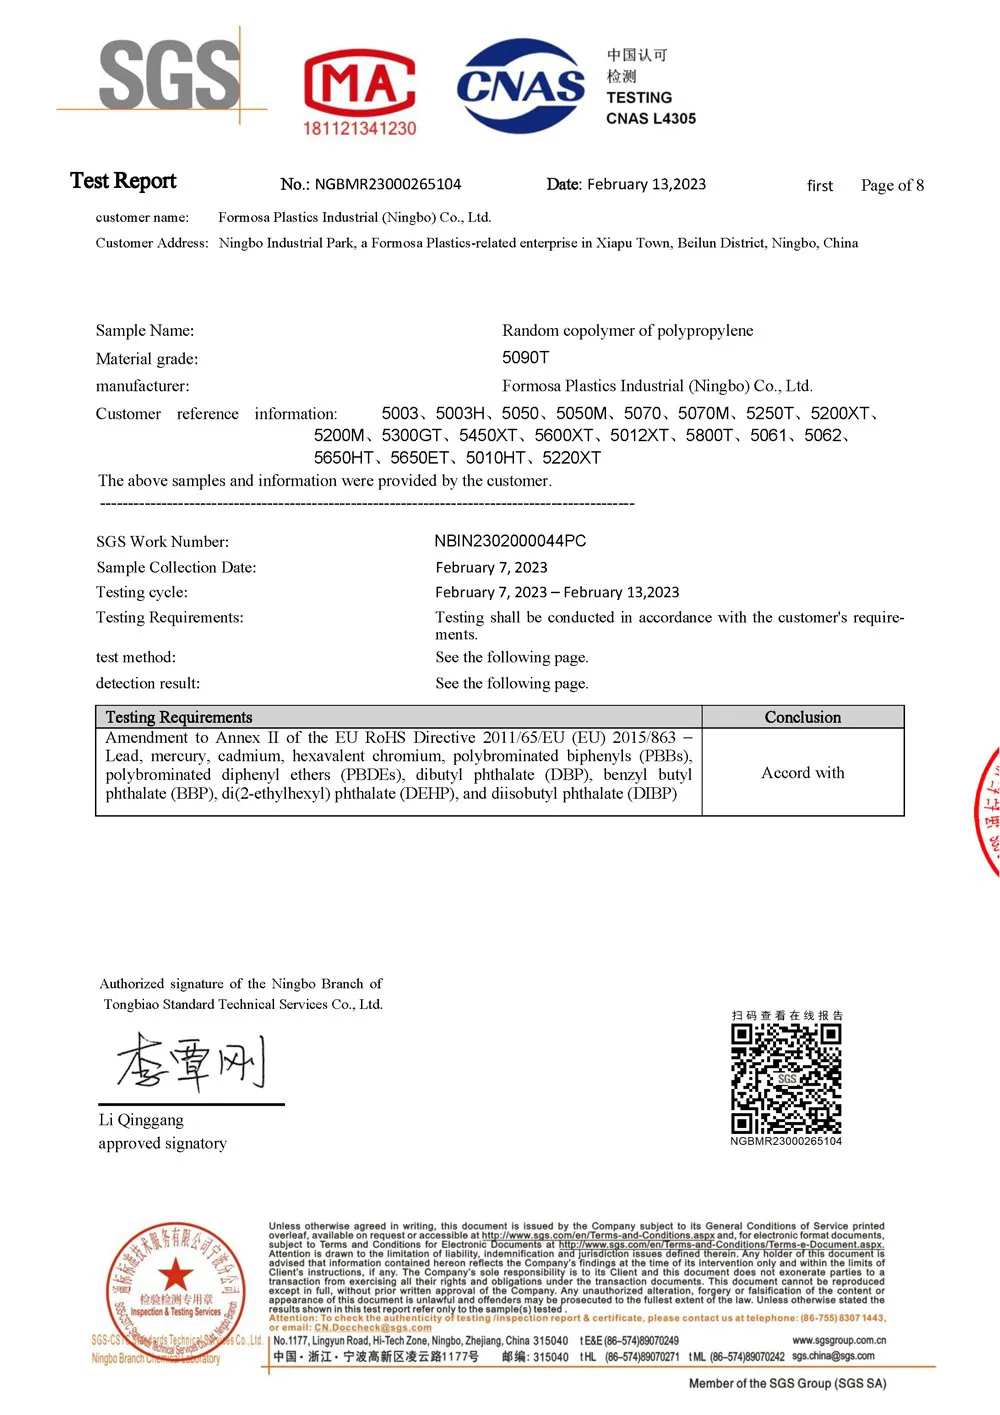
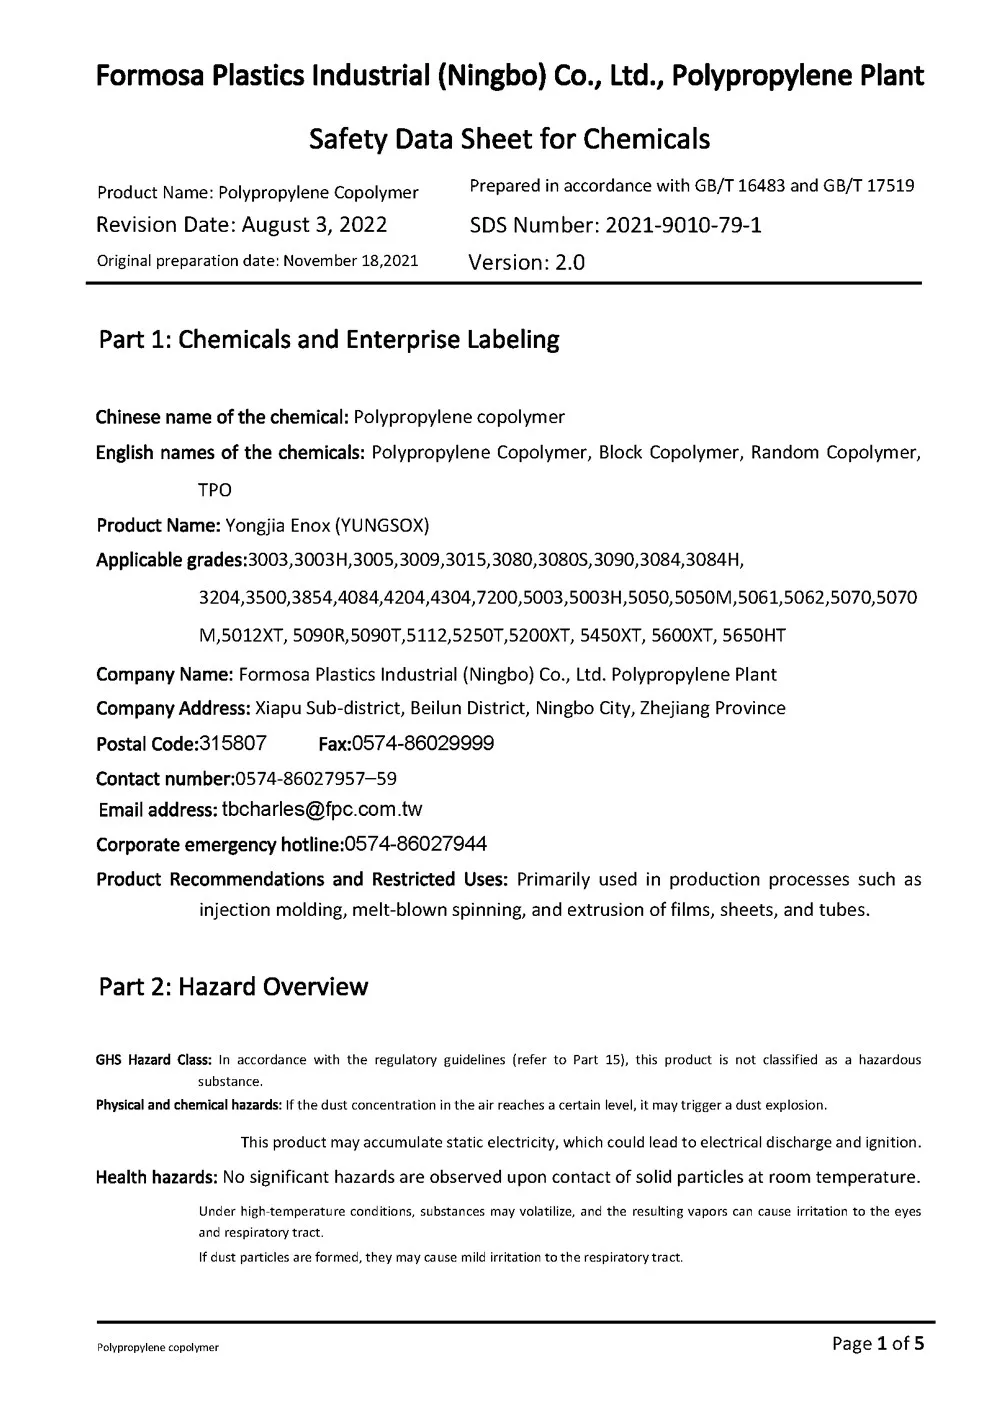
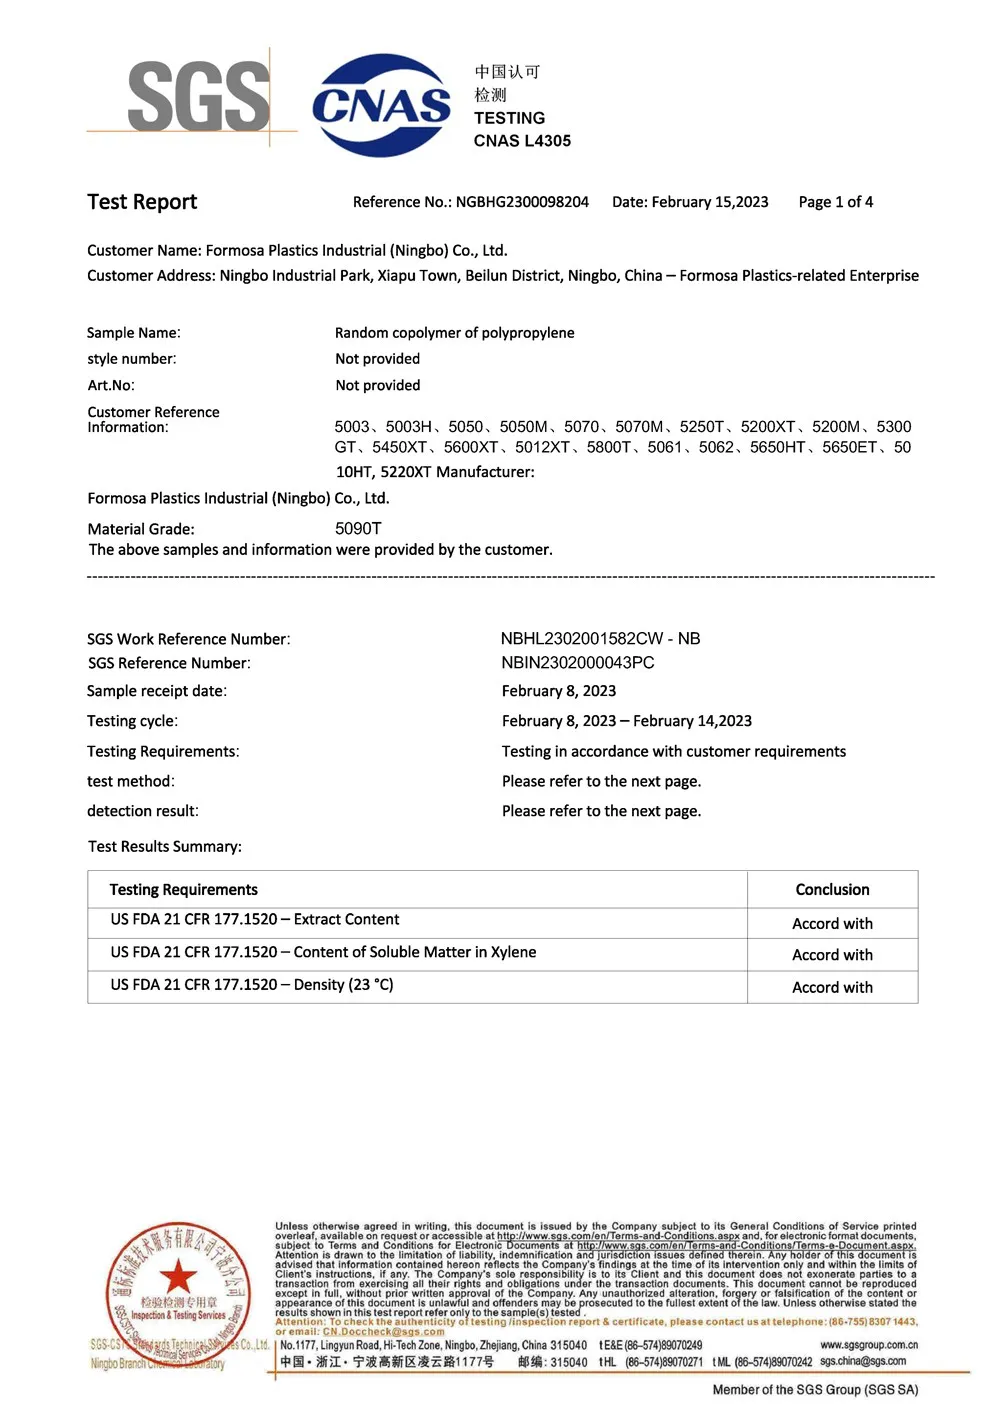
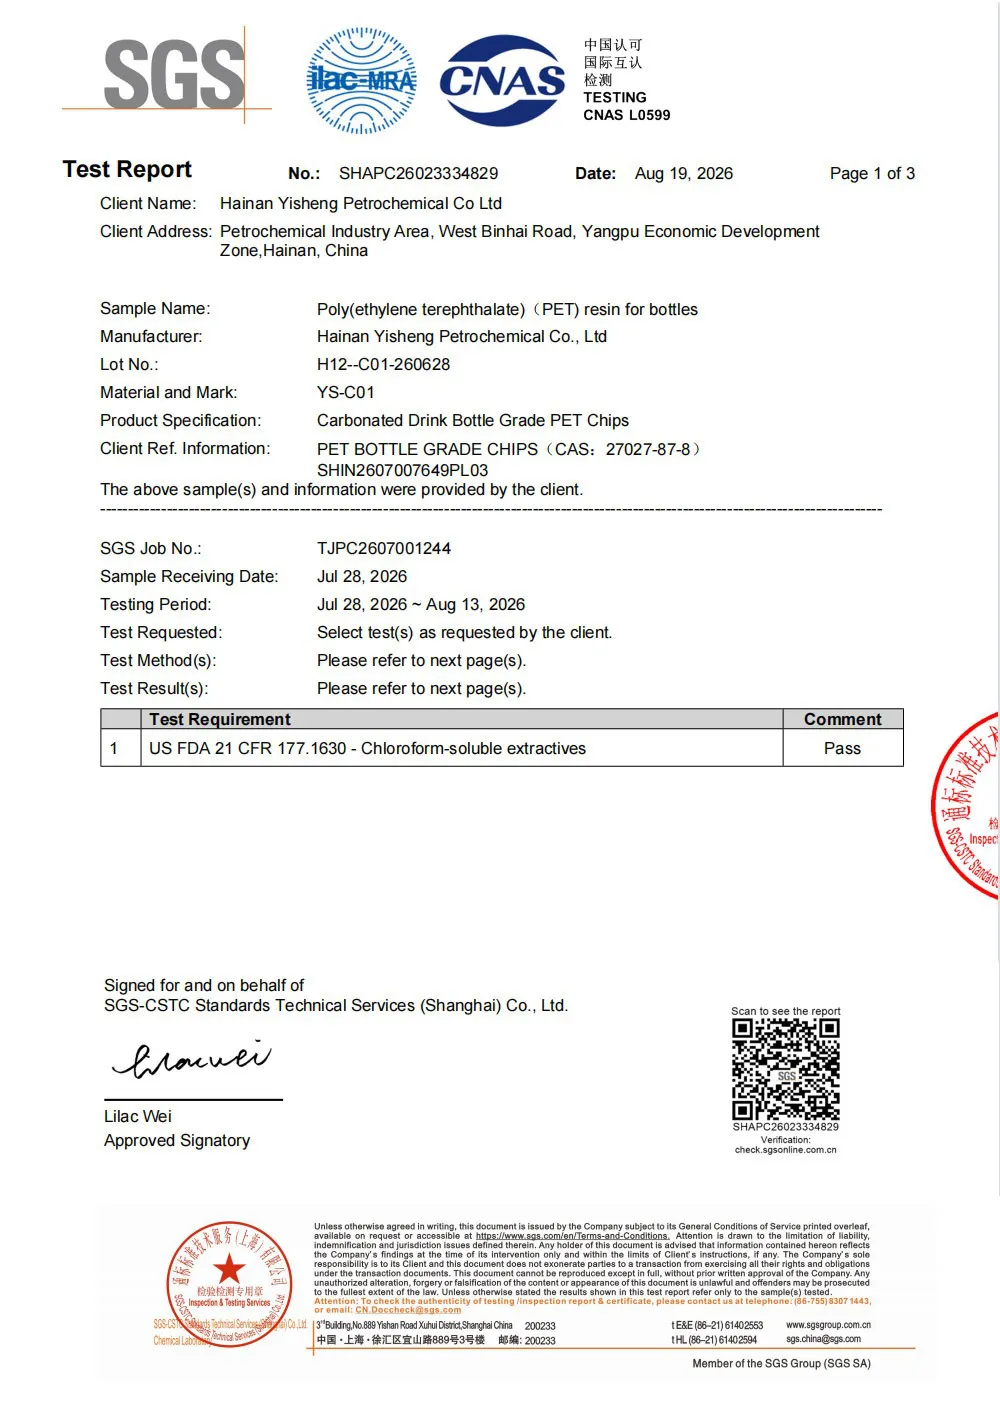
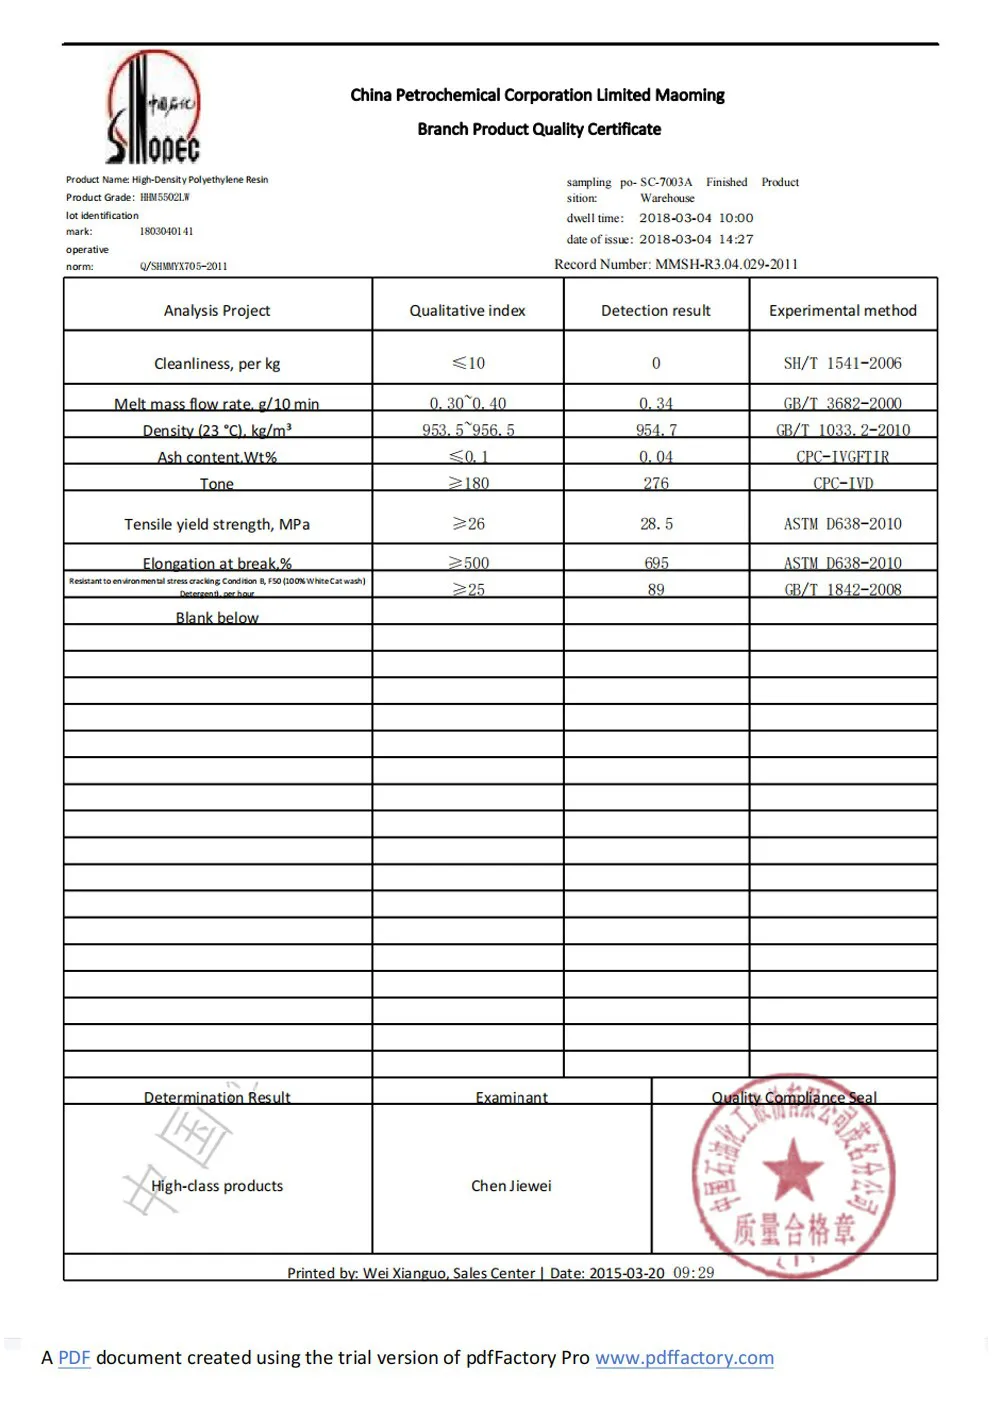
We only use virgin HDPE (High-Density Polyethylene) resin that meets both FDA and EU Pharmacopoeia standards. Why HDPE? It's naturally resistant to moisture, chemicals, and impact – perfect for protecting sensitive medications like vitamins, antibiotics, and herbal supplements. Unlike cheaper plastics that might leach harmful substances, our HDPE is non-toxic, odorless, and won't react with the contents inside. We also offer specialized options, like amber-tinted bottles for light-sensitive drugs or UV-protected variants for medications that degrade in sunlight.
And yes, we test every batch of raw material. Our lab team runs checks for heavy metals, phthalates, and other contaminants before production even starts. Because when you're dealing with products that affect people's health, "good enough" isn't good enough.
Walk into our production campus in Dongguan, and you'll notice something different right away: the air feels cleaner, the floors shine, and every worker wears head-to-toe protective gear. That's because we operate a dust-free GMP compliant workshop specifically designed for pharmaceutical packaging. Our Class 100,000 cleanrooms (that's industry-speak for "really, really clean") ensure no dust, bacteria, or particles contaminate your bottles during manufacturing. We also have separate production lines for medical and cosmetic packaging to avoid cross-contamination – a detail that matters when you're packaging prescription drugs.
But don't just take our word for it. Our facility is audited annually by third-party inspectors, and we're proud to hold ISO 9001:2015 certification – a global standard for quality management systems. This isn't just a certificate on the wall; it's a daily commitment to processes that reduce errors, improve consistency, and ensure every bottle meets the same high bar.
We've all heard the horror stories: curious kids getting into medicine cabinets and accidentally ingesting pills. That's why child-resistant caps (CRCs) aren't just an add-on for us – they're a standard feature on most of our HDPE pill bottles. Our CRCs are designed to be easy for adults to open but tricky for little hands, meeting ASTM D3475 standards (the gold standard for child resistance testing). We even offer "senior-friendly" versions for elderly patients who might struggle with traditional CRCs – because accessibility matters too.
Tamper-evident seals are another non-negotiable. Every bottle we produce comes with a foil liner or shrink band that shows clear signs if it's been opened before. For pharmaceutical companies, this isn't just about compliance – it's about building trust with patients. When someone sees that unbroken seal, they know their medication hasn't been tampered with.
Okay, so we've talked about the "why" – now let's get into the "what." Our HDPE pill bottles come in over 50 standard sizes, from tiny 10ml sample vials to large 500ml bottles for bulk medications. But what really sets them apart is the attention to detail in every design. Let's take a closer look at the features that make our bottles a top choice for pharmaceutical brands worldwide.
We've spent years tweaking our bottle designs based on feedback from pharmacists, patients, and drug manufacturers. Here are a few "small" details that our clients love:
We get it – your medication is unique, so your packaging should be too. As a custom plastic bottle manufacturer , we don't believe in "one-size-fits-all" solutions. Whether you need a bottle that matches your brand colors, a unique shape that stands out on shelves, or specialized printing for dosage instructions, we've got you covered. Let's walk through how we turn your vision into reality.
Ever had an idea for a bottle shape that's never been done before? Our in-house mold design team lives for that challenge. We start with your 3D (or even just a sketch on a napkin!) and use CAD software to create a digital prototype. Once you approve the design, we build a test mold – and here's the best part: we offer free mold testing to make sure the bottle works exactly how you want before mass production. No hidden fees, no surprises.
We've designed molds for everything from eco-friendly "square-round" bottles (they stack better and use 15% less plastic!) to bottles with built-in pill counters. And because we build our own molds, we can make tweaks quickly if something isn't quite right. Most mold projects are ready for sampling in 2-3 weeks – way faster than the industry average of 4-6 weeks.
Your pill bottle is a marketing tool too – and it should reflect your brand's values. We offer a range of printing and branding options to make sure your bottle stands out:
We also handle all the regulatory fine print – like batch codes, expiration dates, and dosage instructions. Our design team is familiar with FDA and EU labeling requirements, so you can rest easy knowing your bottle meets all compliance standards.
Here's a pet peeve we hear from new pharmaceutical brands: "Most manufacturers require 100,000 bottles minimum, but we're just starting out!" We get it – not every brand needs a million bottles right away. That's why we offer flexible minimum order quantities (MOQs). For standard sizes, we can start as low as 5,000 units. For custom molds, MOQs are higher (usually 20,000+), but we'll work with you to find a solution that fits your budget and growth plans. We've helped dozens of startups launch their first product, and there's nothing more rewarding than seeing them come back a year later needing 10x the order.
While HDPE pill bottles are our claim to fame, we're more than just a "pill bottle company." We offer a full range of medical-grade packaging solutions for pharmaceutical and healthcare brands. Let's take a quick tour of some of our other products that keep medications safe and effective.
If you work in a lab or biotech company, you know how critical it is to store samples safely at ultra-low temperatures. Our cryogenic tubes (or "cryo tubes") are designed to withstand liquid nitrogen temperatures (-196°C) without cracking or leaking. Made from high-quality polypropylene (PP), they come with silicone gaskets for an airtight seal – no more worrying about sample contamination during storage. We offer sizes from 0.5ml to 5ml, with internal or external threads, and even barcoded options for easy sample tracking. Whether you're storing blood samples, cell cultures, or vaccines, our cryo tubes are trusted by research labs across Europe and North America.
Not all medications come in pill form. We also produce HDPE bottles for liquid meds like cough syrups, eye drops, and oral suspensions. These bottles feature precise pour spouts to prevent spills, and some come with calibrated droppers or measuring cups for accurate dosing. We even offer child-resistant caps for liquid medications – because safety shouldn't depend on the form of the drug.
Here's a secret about the packaging industry: not every manufacturer tests their products as rigorously as they should. But for us, quality control isn't a "step" – it's the entire process. From the moment raw plastic resin arrives at our factory to the second your bottles are loaded onto a truck, we're testing, inspecting, and double-checking. Let's pull back the curtain on how we ensure every bottle meets our standards.
We only source resin from trusted suppliers who provide certificates of analysis (COAs) for every batch. But we don't stop there – our lab team runs additional tests for:
If a batch fails any test, we send it back – no exceptions. Because garbage in = garbage out, and we don't do garbage.
During production, our operators check bottles every 30 minutes. They're looking for:
We also use automated cameras to inspect bottles for defects that the human eye might miss – like tiny cracks or inconsistent coloring. If the camera flags an issue, the production line stops automatically until we fix the problem.
Before bottles are packed, they go through a battery of final tests:
Only about 99.5% of bottles pass all these tests – the other 0.5% get recycled (we hate waste!). But that 99.5%? They're perfect.
Let's talk about plastic and the planet. We know there's a lot of concern about plastic waste, and we're committed to doing our part to make pharmaceutical packaging more sustainable. Here's how we're working to reduce our environmental footprint – without compromising on safety or quality.
For brands looking to reduce their carbon footprint, we offer bottles made with post-consumer recycled (PCR) HDPE. Our PCR plastic is sourced from recycled milk jugs and detergent bottles, cleaned thoroughly, and processed to meet medical-grade standards. PCR bottles have the same strength and chemical resistance as virgin HDPE, but they use 70% less energy to produce and reduce landfill waste. We currently offer PCR options for non-sterile medications and supplements, and we're working on sterile PCR solutions for prescription drugs.
Another way we reduce plastic use is through "lightweighting" – designing bottles with thinner walls that still meet strength requirements. Our engineering team uses finite element analysis (FEA) to identify areas where we can remove plastic without weakening the bottle. For example, our 60ml pill bottle used to weigh 12g; now it weighs 10g – that's 17% less plastic per bottle, and we've maintained the same drop-test performance. Over a million bottles, that's 20,000kg less plastic in the world!
Sustainability isn't just about the product – it's about how we make it. We've invested in solar panels that power 30% of our factory, and we use energy-efficient motors on all our production equipment. We also recycle 90% of our water used in cooling processes, and we've reduced our overall water consumption by 25% in the last 5 years.
At the end of the day, pharmaceutical packaging isn't just about plastic and caps. It's about protecting patients, building trust, and supporting the work of healthcare professionals who rely on safe, reliable medications. For 18 years, we've approached every bottle with that mindset – and it's why global pharmaceutical firms keep coming back.
Whether you need standard HDPE pill bottles, custom-designed containers, or help navigating regulatory requirements, we're here to make your life easier. We're not just a supplier – we're a partner who's invested in your success.
So let's talk. Tell us about your product, your goals, and your challenges. We'll help you find a packaging solution that's safe, reliable, and designed to make your brand shine. After all, when your medication reaches patients, we want them to feel the same confidence in your packaging that you feel in your product.