Email: info@mggpacking.com | Tel: +86-13510174848 ( Mr. Yao)


In the world of pharmaceuticals, every detail counts—from the active ingredients in a pill to the bottle that holds it. For patients, a medication bottle is more than just a container; it's a promise of safety, freshness, and reliability. For pharmaceutical companies, choosing the right packaging isn't just a logistical decision—it's a commitment to protecting the integrity of their products and the trust of the people who depend on them. That's where the 225ml GMP certified HDPE pill bottle comes in: a workhorse of pharmaceutical packaging designed to meet the rigorous demands of the industry while ensuring medications stay potent and secure from production to patient.
As a leading pharmaceutical packaging manufacturer , we understand that (pharmaceutical packaging) is the unsung hero of healthcare. It guards against moisture, light, and contamination; prevents accidental ingestion, especially by children; and ensures dosages remain accurate even after repeated use. And when it comes to balancing durability, safety, and cost-effectiveness, few materials stand out like High-Density Polyethylene (HDPE)—the material at the heart of our 225ml pill bottles.
Not all plastics are created equal, especially when lives are on the line. HDPE, or High-Density Polyethylene, has long been the gold standard for medical and pharmaceutical packaging—and for good reason. Its unique properties make it ideal for storing everything from vitamins and supplements to prescription medications that require long-term stability.
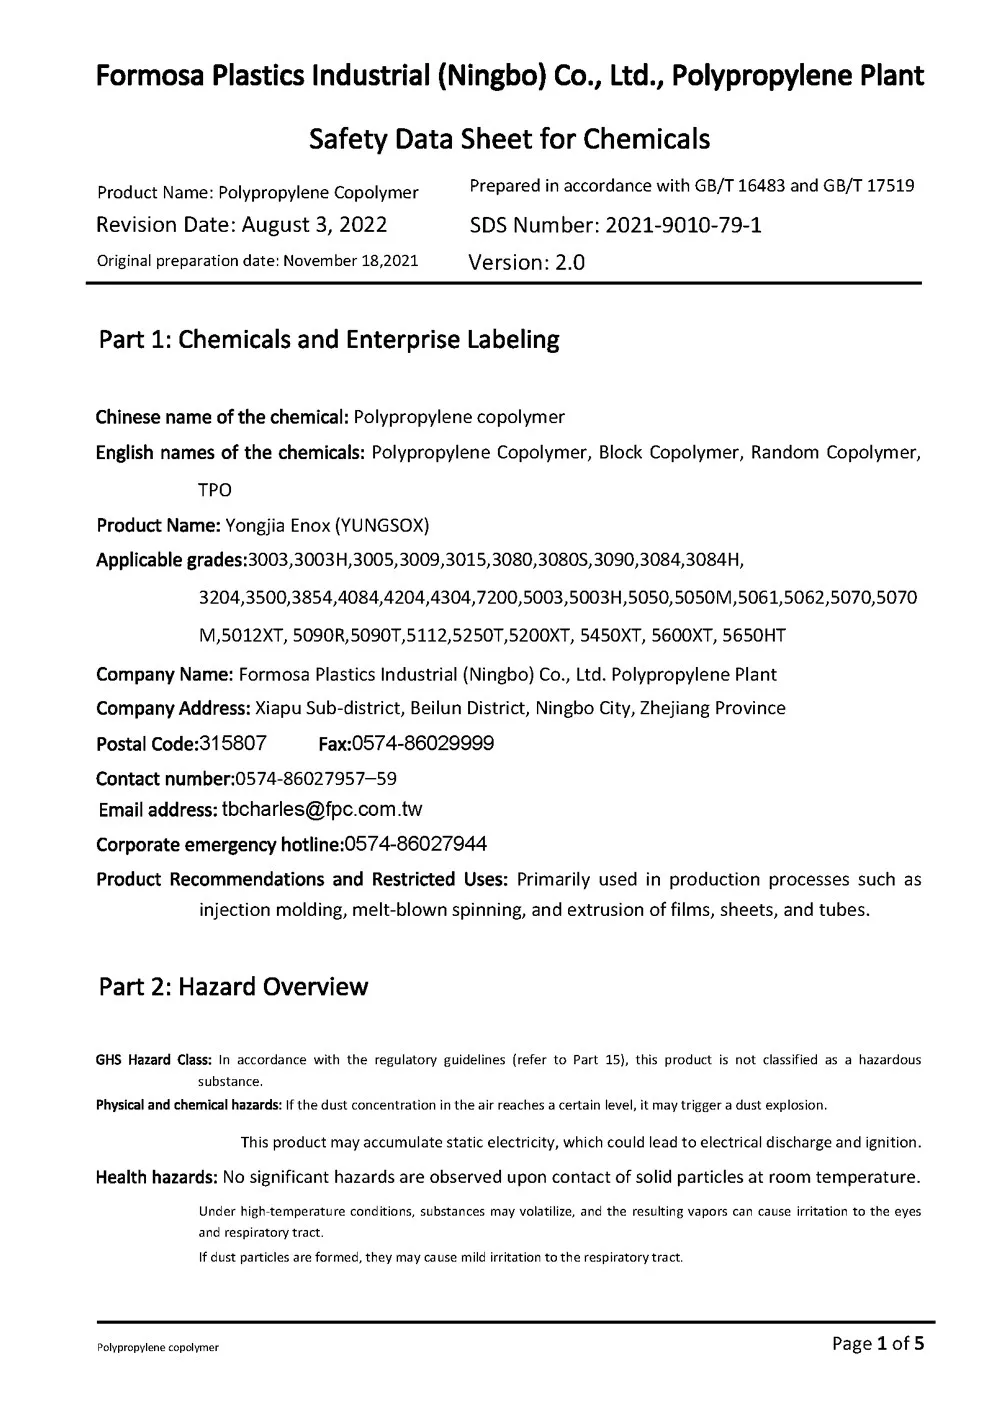
First, HDPE is inherently resistant to chemicals, which means it won't react with the medications inside. Whether you're packaging aspirin, antibiotics, or herbal supplements, you can trust that the bottle won't leach harmful substances or alter the medication's composition. This chemical inertness is why HDPE is the top choice for medical grade plastic bottles worldwide.
Second, HDPE is moisture-resistant. We've all heard the warning: "Keep this medication in a cool, dry place." That's because moisture is a medication's worst enemy, capable of breaking down active ingredients and reducing efficacy. HDPE's tight molecular structure acts as a barrier, keeping humidity out and ensuring pills, capsules, and tablets stay dry and potent for their full shelf life.
Third, HDPE is durable yet lightweight. Unlike glass, which is heavy and prone to shattering, HDPE bottles can withstand the bumps and drops of shipping and handling without compromising the product inside. This durability makes them a favorite for wholesale and bulk distribution, where packages are often stacked, transported, and stored in warehouses before reaching pharmacies or patients.
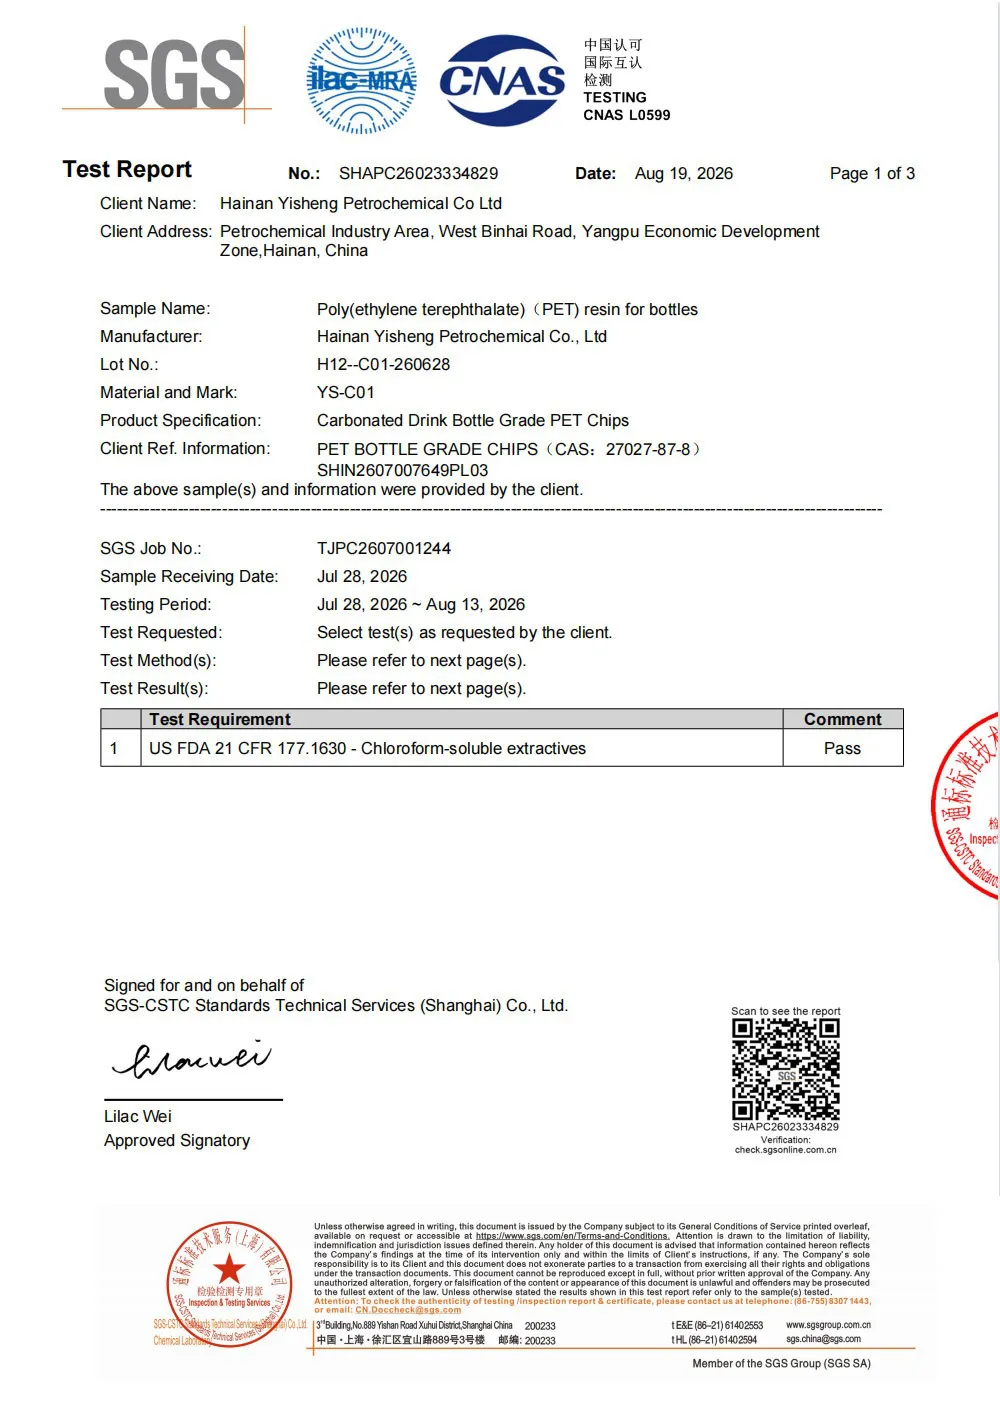
When it comes to pharmaceutical packaging, "good enough" isn't enough. That's why our 225ml HDPE pill bottles are manufactured in a dust-free GMP compliant workshop and carry the ISO 9001:2015 certification. But what do these terms really mean for you and your customers?
GMP, or Good Manufacturing Practices, is a set of strict guidelines enforced by regulatory bodies worldwide to ensure products are consistently produced and controlled according to quality standards. For a packaging factory, GMP compliance means every step of the process—from raw material sourcing to production and testing—is monitored and documented. Our workshop operates in a controlled environment with air filtration systems to minimize dust and contamination, and all equipment is regularly sanitized to meet pharmaceutical-grade requirements. This isn't just about following rules; it's about ensuring that every bottle that leaves our facility is free from impurities that could compromise the medications it holds.
ISO 9001:2015 certification takes this a step further by focusing on quality management systems. It means we've implemented processes to continuously improve our operations, from reducing waste to enhancing customer satisfaction. When you partner with an ISO 9001 certified packaging factory , you're not just buying a product—you're investing in a supply chain that prioritizes consistency, reliability, and accountability.
| Certification | Key Focus | Benefit to Customers |
|---|---|---|
| GMP Compliance | Dust-free production, contamination control, strict hygiene standards | Medication safety and purity |
| ISO 9001:2015 | Quality management, process optimization, continuous improvement | Consistent product quality, reliable supply |
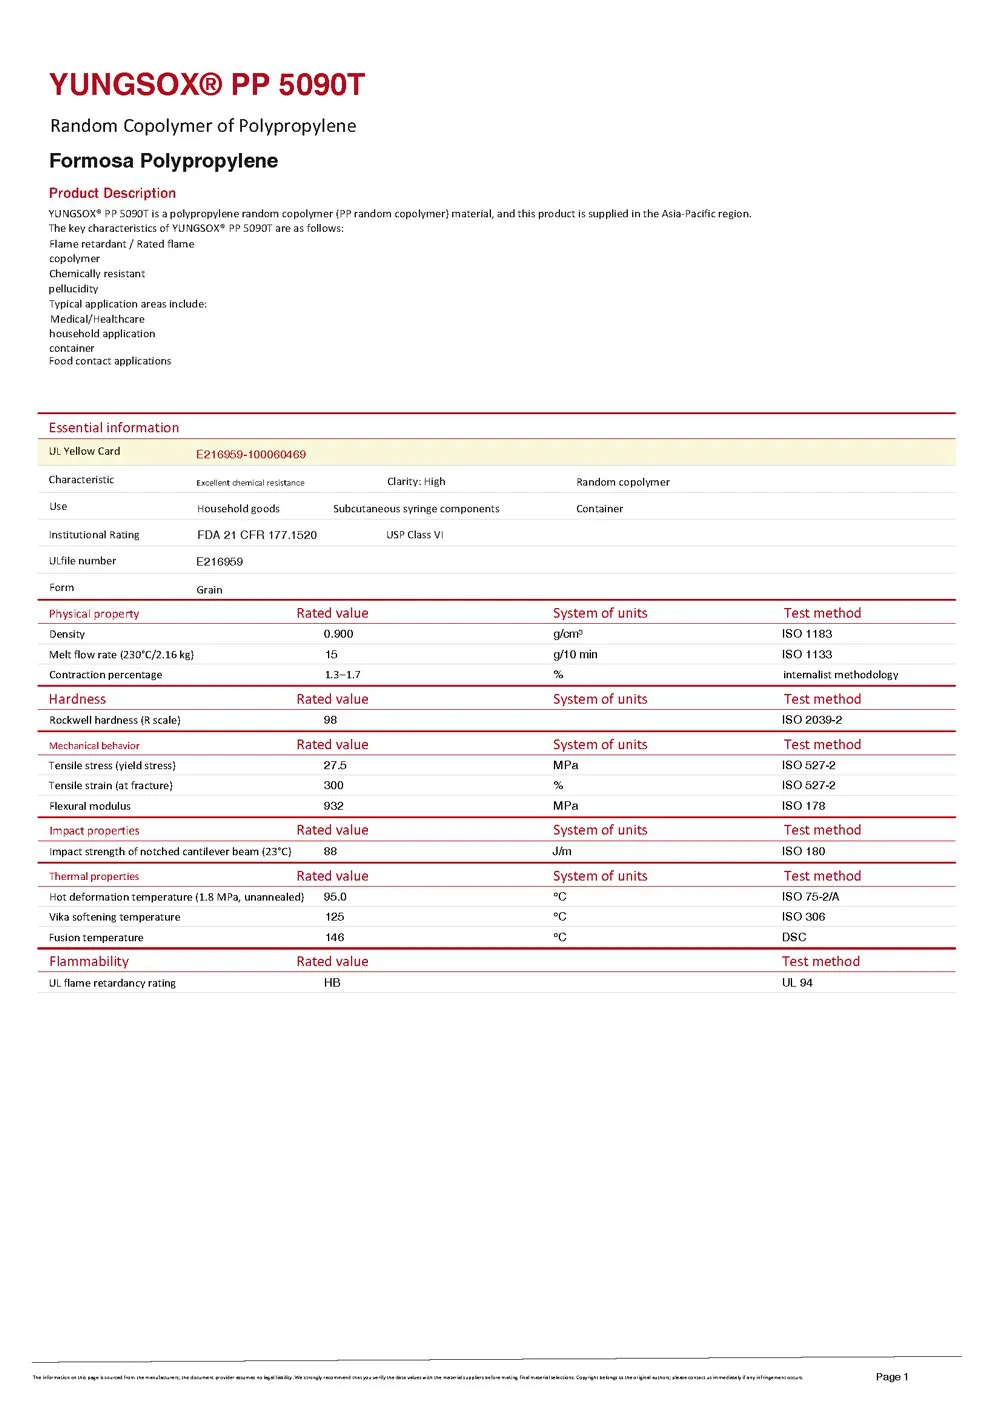
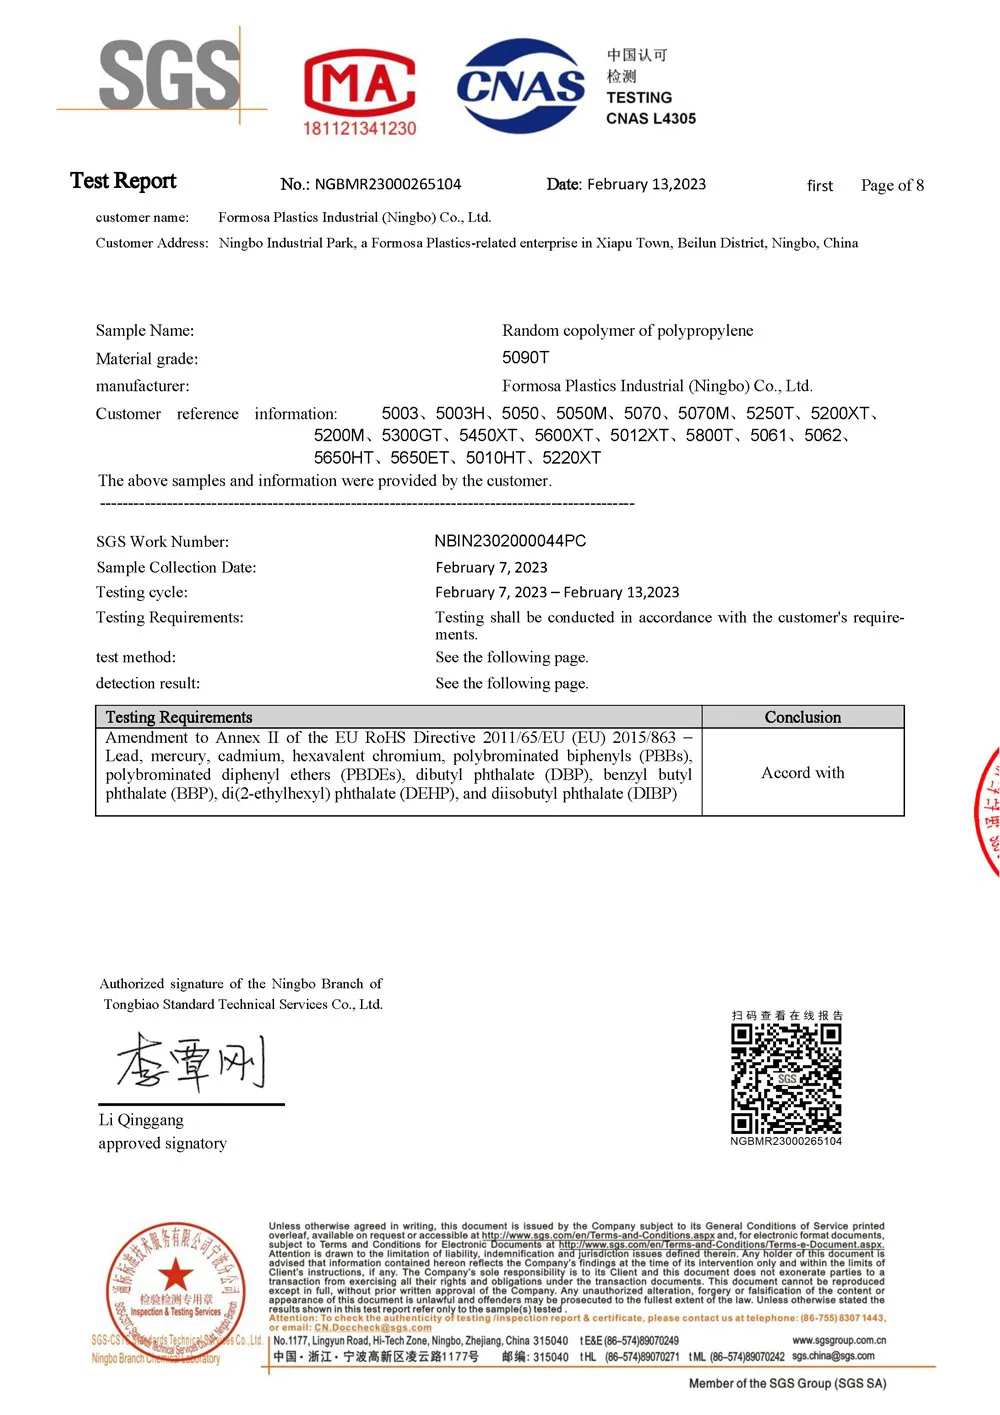
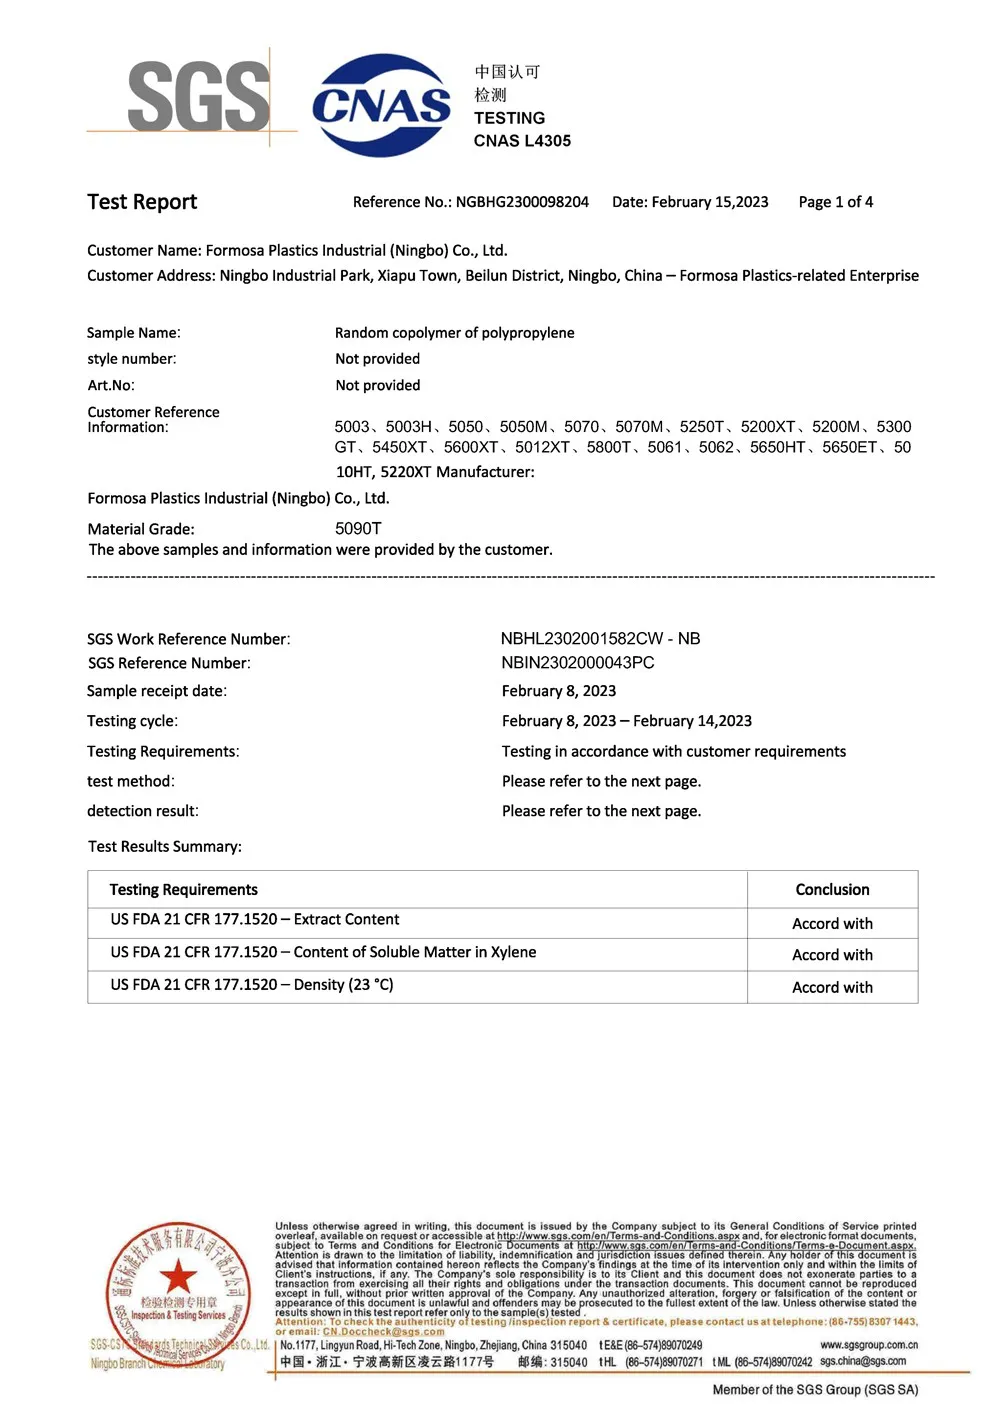
| Food-Grade & Medical-Grade Standards | Material safety, non-toxicity, chemical resistance | Peace of mind for patients and regulators |
The 225ml size isn't arbitrary—it's a sweet spot for pharmaceutical packaging. It's large enough to hold a month's supply of most medications (think 30-60 tablets, depending on size) but compact enough to fit in medicine cabinets, purses, or travel bags. Whether you're a pharmacy looking to stock standard prescription bottles or a supplement brand needing bulk packaging, the 225ml HDPE pill bottle offers versatility without sacrificing functionality.
Let's break down its key features:
But don't just take our word for it. As an hdpe pill bottles supplier with years of experience, we've worked with pharmaceutical companies, supplement brands, and veterinary clinics to refine this design based on real-world feedback. The result? A bottle that checks all the boxes: safe, durable, user-friendly, and cost-effective.
While our 225ml HDPE pill bottle is a standout on its own, we understand that every brand and product is different. That's where our custom capabilities shine. As a custom plastic bottle manufacturer , we don't believe in one-size-fits-all packaging. Whether you need a unique color, a custom cap, or even a modified bottle shape, we can bring your vision to life.
| Custom Service | What We Offer | Why It Matters |
|---|---|---|
| Mold Design & Manufacturing | 3D (3D drawing customization), free mold testing, rapid prototyping | Create unique bottle shapes that stand out on shelves |
| Color Matching | Pantone color matching for bottles and caps | Align packaging with your brand's color scheme for instant recognition |
| Logo & Branding | Embossed logos, silk-screen printing, hot stamping | Add a premium, professional touch that builds brand trust |
| Cap Customization | Child-resistant, senior-friendly, or custom closure designs | Tailor usability to your target audience (e.g., easy-open caps for elderly patients) |
Our custom process is straightforward: share your requirements (whether it's a sketch, 3D file, or just an idea), and our team of engineers will work with you to develop a prototype. We offer free mold testing to ensure the design works before full production, minimizing risk and ensuring you get exactly what you need.
In today's world, sustainability isn't an afterthought—it's a priority. We're committed to reducing the environmental impact of plastic packaging without compromising on quality. Our 225ml HDPE pill bottles are fully recyclable, and we offer options for using PCR (Post-Consumer Recycled) HDPE, which gives new life to plastic waste. Additionally, we optimize our manufacturing processes to minimize material waste and energy use, ensuring that every bottle is produced as efficiently as possible.
We also understand that sustainability goes beyond materials. That's why we offer lightweight bottle designs that reduce shipping costs and carbon emissions, and we work with customers to find the right balance between durability and material usage—so you get a bottle that's strong enough to protect your product but doesn't use more plastic than necessary.
The pharmaceutical packaging market is crowded, but not all suppliers are created equal. Here's what sets us apart:
At the end of the day, pharmaceutical packaging is about more than plastic and caps. It's about protecting the medications that keep people healthy, the brands that work tirelessly to develop them, and the trust between patients and providers. The 225ml GMP certified HDPE pill bottle is a testament to that commitment: a product designed with safety, reliability, and functionality at its core.
Whether you're looking for bulk wholesale bottles, custom-designed packaging, or a partner who understands the unique demands of the pharmaceutical industry, we're here to help. Because when it comes to something as important as medication packaging, you deserve the best.